
NewsDetails
Fuel Oil Booster Pump Stations — Design and Operation for Industrial Facilities
author:Tianyi Pump time:2026-08-20 11:55:00 Click:65
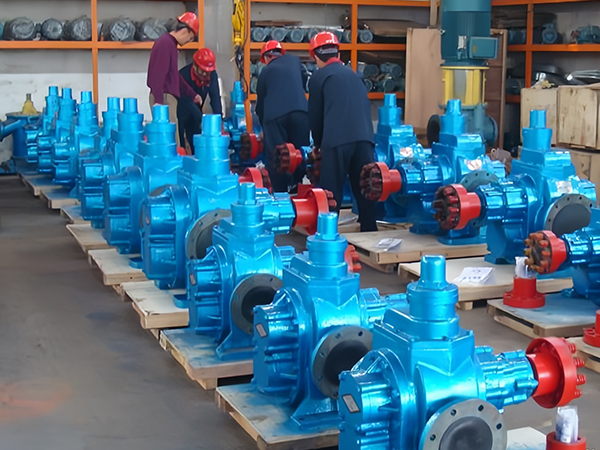
Industrial facilities that burn fuel oil — power plants, refineries, chemical factories, and large commercial buildings — all share a common need: a reliable system to receive, store, condition, and deliver fuel to the burners or boilers. The fuel oil booster pump station is the mechanical heart of this system. It draws fuel from storage tanks, raises the pressure to overcome burner requirements, and often heats the fuel to reduce viscosity for proper atomization. A well-designed booster station ensures stable combustion, protects burner equipment, and reduces fuel consumption. Working with an experienced fuel pump manufacturer to specify the correct booster station components prevents the performance problems that arise when marginal equipment is specified for demanding fuel oil service.
Understanding Fuel Oil Booster Pump Requirements
Fuel oils range from light distillates similar to diesel to heavy residual fuels with viscosities exceeding 1000 centistokes at ambient temperature. A booster pump must handle the specific gravity, viscosity, and temperature of the fuel being burned. The pump must also overcome the pressure drop across strainers, fuel heaters, and burner nozzles to deliver fuel at the required atomization pressure. For heavy fuels, the pump must continue functioning as the fuel is heated to 100-180 °C in the preheater train — at these temperatures, the fuel has lower viscosity but the pump seals and bearings are exposed to elevated temperatures. A competent fuel pump supplier specifies materials and seals appropriate to the actual operating temperature, not just the nominal rating.
Single-Pump and Dual-Pump Configurations
Small facilities with stable fuel demand may use a single booster pump sized for the maximum burner flow at design conditions. Most commercial and industrial installations use dual pumps arranged in parallel, with one pump running and one on standby. This arrangement allows pump swap-over without interrupting combustion, and permits one pump to carry base load while the second handles peak demand. The parallel arrangement requires check valves on each pump discharge to prevent backflow through the idle pump. Control systems sequence pump start-stop based on line pressure, maintaining a nearly constant discharge pressure even as the number of active burners fluctuates throughout the day.
Viscosity Management and Fuel Heating
For heavy fuel oils, viscosity management is as important as pressure management. Heavy fuels must be heated to reduce viscosity to a level where the burner can atomize the fuel into fine droplets. Typical atomization viscosity for residual fuel is 15-25 centistokes, requiring fuel temperatures of 130-180 °C depending on the fuel grade. The booster pump sits upstream of the fuel heater in the system sequence: cold fuel is drawn from the storage tank, pressurized by the pump, and then passed through the heater before reaching the burners. Installing the pump before the heater protects it from the thermal stress of hot fuel, though seals must still tolerate occasional temperature excursions during heater malfunction. Some fuel pump factories offer pumps with integral heating jackets for applications where the pump must handle hot fuel directly.
System Protection and Redundancy
A fuel oil booster station must include adequate protection against the abnormal conditions that occur in every plant over time. Low suction pressure protection prevents the pump from running with an empty or air-bound suction line, which rapidly damages gear pump bearings and shafts. High discharge pressure protection — a relief valve set below the maximum working pressure of downstream equipment — prevents overpressure damage if a burner valve fails in the closed position. The suction strainer must be cleaned regularly; a blocked strainer reduces flow and causes cavitation, evidenced by unusual pump noise and vibration. A responsible fuel pump manufacturer provides a complete system datasheet showing maximum and minimum operating conditions, NPSH required, and recommended materials for the specified fuel grade.
Commissioning and Ongoing Performance
A newly installed fuel oil booster station must be commissioned with particular attention to the purging of air from the suction line and pump casing before startup. Air pockets in the suction line prevent the pump from priming and produce erratic discharge pressure. After start-up, the operator should verify that discharge pressure is stable, that both pumps can carry the full load independently, and that automatic transfer to the standby pump activates correctly on loss of pressure. Ongoing performance monitoring — recording discharge pressure, suction strainer differential pressure, and motor current — builds a baseline that makes it easy to identify when the pump is beginning to wear. An experienced fuel pump supplier offers commissioning support and can provide replacement wear parts including bearings, shafts, and gear sets to restore the pump to original performance after years of demanding service.
References
Bloch, H. P., & Budris, A. R. (2013). Pump User's Handbook: Life Extension (4th ed.). Fairmont Press.
Karassik, I. J., Messina, J. P., Cooper, P., & Heald, C. C. (2001). Pump Handbook (4th ed.). McGraw-Hill.
Nesbitt, B. (2006). Handbook of Pumps and Pumping. Elsevier.
Combustion Engineering Association. (2011). Fuel Oil Pumping and Heating Systems. CEA Technical Guide No. 7.
Brennen, C. E. (1994). Hydrodynamics of Pumps. Cambridge University Press.
 Recommended Products
 Contact us
—— Contact:Mr. Shi
—— Tel:+86 15612730683
—— Email:btclyb@163.com
—— Url:https://www.tianyi-pump.com
—— Address:260 meters east of Xiaoquan Village Committee, Bozhen, Botou City, Cangzhou City, Hebei Province